A production line becomes difficult to control when motors, valves, sensors and safety devices operate as disconnected components. By the end, you will be able to trace each device through a coordinated control sequence, identify the safety functions that need dedicated hardware, and prepare a clearer panel design brief.
Key takeaways
- Use PLC interlocks to prevent machines from running out of sequence.
- Assign each drive clear duties for speed, torque, overload and fault reporting.
- Separate emergency stopping from ordinary PLC logic with safety-rated functions.
- Map sensors, actuators, permissives and fault responses before specifying the panel.
How a PLC panel turns separate machines into one coordinated process
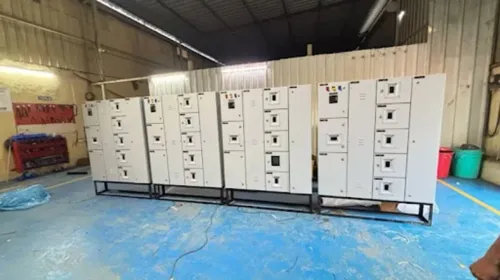
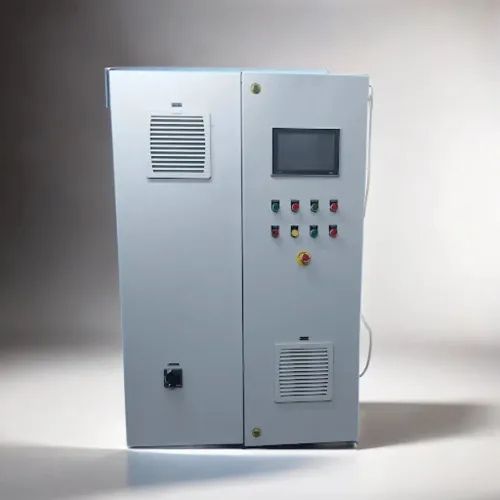
A PLC panel turns separate machines into one coordinated process by reading sensors, evaluating interlocks and sequencing logic, then sending commands to actuators. The industrial control panel becomes the line’s decision point: it knows whether upstream material is available, whether the next machine is ready and whether a fault has stopped safe operation.
1. The PLC checks permissives before issuing a start command. These can include a closed guard or mixer lid, available discharge path, correct valve position, adequate tank level, no overload and no emergency-stop condition.
2. It starts equipment in order and passes handshakes between machines. A conveyor will not run until its guard switch is closed and the receiving machine reports ready; a pump will stop when a low-level sensor signals loss of suction.
3. It confirms action through feedback. A motor starter auxiliary contact, valve-position switch or speed signal tells the PLC whether the commanded actuator actually responded. A failed feedback signal creates a specific fault instead of a misleading “not ready” message.
4. It records and displays alarms with their causes, allowing operators to correct the failed permissive rather than repeatedly pressing Start.
5. A normal stop completes controlled valve closure, pump rundown or agitator deceleration. An emergency stop addresses hazardous motion through a safety-rated circuit; ordinary PLC logic and a conventional ready bit do not replace that function.
After power returns, the PLC should require a deliberate restart and recheck every permissive. Servicing still requires lockout/tagout and zero-energy verification, including pneumatic, hydraulic, thermal and gravitational energy.
What each panel and drive is responsible for
The PLC panel owns the production decision: it checks permissives, runs the sequence, exchanges ready and running signals, records faults, and issues commands. It does not automatically own every protection function. A guard-door stop or emergency stop must use a safety architecture that meets the risk assessment’s required Performance Level under ISO 13849-1.
| Equipment | Primary responsibility | Coordination boundary |
|---|---|---|
| PLC panel | Sequence logic, interlocks, alarms, timers, and equipment handshakes | Requests operation and interprets feedback; it does not replace safety-rated circuits |
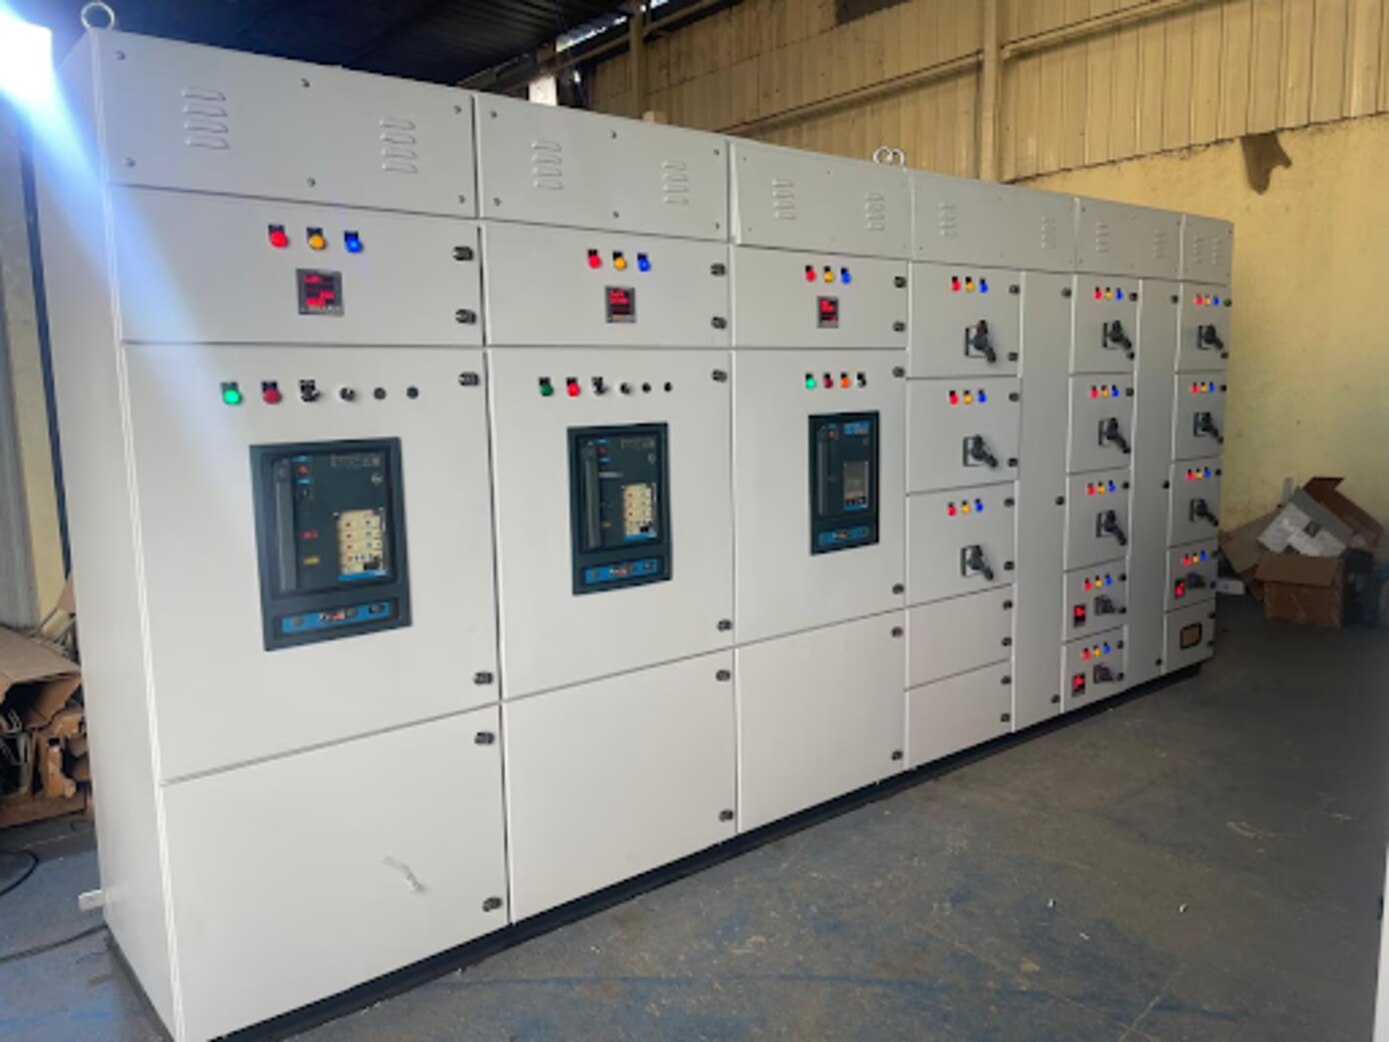
| MCC panel | Motor starting, isolation, overload protection, and motor branch control | Supplies controlled motor operation; the overload setting must match the motor and application |
| PCC panel | Incoming power, busbars, feeders, switching, and short-circuit or earth-fault protection | Distributes electrical power; it does not decide process order or motor speed |
| APFC panel | Automatic power-factor correction through capacitor stages and switching control | Reduces reactive demand; it does not control a mixer’s speed or sequence |
| VFD system | Motor frequency, speed, acceleration, deceleration, and torque control | Executes the PLC’s speed command and reports status, trips, and feedback |
Treat a VFD system as the speed-control layer, not as proof that a motor is safe to run. A conventional PLC “ready” bit can fail silently, so a safety-critical inter-machine dependency belongs in the validated safety function. Record specific states such as “drive fault,” “overload trip,” and “low level,” rather than displaying only “motor unavailable.”
How a safe start, run, trip and restart sequence works
A safe sequence treats a start request as a request to check conditions, not permission to energise every motor. The PLC evaluates permissives, exchanges equipment handshakes, issues commands in order, and confirms feedback before advancing.
1. The operator presses Start. The PLC checks that the emergency stop circuit is reset, guards and lids are closed, the discharge path is available, valves are in the commanded positions, level is adequate, and no overload, short-circuit or drive fault is active.
2. The PLC sends a run-permit handshake to the relevant drive or motor starter. The device returns “ready” feedback; without it, the sequence stops at that step and displays the failed permissive, not just “not ready.”
3. The PLC starts supporting equipment in order. A pump may start before an agitator, while a high-inertia mixer uses a drive ramp, reduced speed or a delay between motors. The PLC then verifies running feedback, pressure, flow or speed before continuing.
4. A missing feedback signal, overload trip, overpressure signal or drive fault removes the run command, records the fault and brings connected equipment to a defined safe state. Do not bypass the overload to prevent nuisance trips.
5. An emergency stop removes hazardous motion through the safety-rated stop circuit. Resetting it must not restart the machine; normal stopping remains separate so valves close, pumps run down and the batch sequence ends predictably.
6. After power returns, an under-voltage release drops contactors and the PLC keeps a restart inhibit active. Require fresh permissives, valid feedback and a deliberate Start command after the operator checks the line.
Which safety functions need more than ordinary PLC logic
A standard PLC controls production: it sequences valves, starts motors, checks levels and reports faults. A safety function protects people from hazardous energy, so the risk assessment—not the presence of a PLC—sets its required Performance Level under ISO 13849-1.
Use a safety relay or safety PLC when the assessed function needs monitored inputs, fault detection or a defined safe output state.
| Function | Normal control role | Safety distinction |
|---|---|---|
| Guard monitoring | Stops a sequence when a door is open | Monitors safety-rated switches and prevents hazardous motion; ordinary input logic is insufficient when the risk assessment requires a PL |
| Overload protection | Trips a motor overload relay | Protects the motor from sustained excess current; do not raise its setting to stop nuisance trips, and add a safety stop when hazardous motion must end |
| Short-circuit protection | Opens a fuse or circuit breaker during a high-current fault | Protects conductors and equipment; it does not replace a controlled machine stop |
| Earth-fault protection | Detects leakage or fault current | Disconnects dangerous electrical faults; select the device and disconnection method for the earthing system and risk |
| Unexpected-start prevention | Restarts sequences after conditions return | Requires deliberate reset and separate start command after power loss or safety-trip reset |
IEC 60204-1 distinguishes normal stopping from emergency stopping and addresses unexpected start-up. A reset must not restart an agitator, conveyor or pump. Verify contactor feedback, dual-channel wiring where required, and the actual coast-down time; a safety circuit cannot compensate for a wrongly wired guard switch or motion that continues after power removal.
How to map the line before choosing or specifying a panel
Do not specify a panel from a motor list alone. Map every motor and field device to its process duty, electrical data, normal state, failure state and safe response before selecting starters, drives, I/O or enclosure space.
Record these fields for each motor:
- Tag, equipment served, kW or horsepower, voltage, full-load current, phase, duty cycle and starting method
- VFD or starter details, rotation requirement, acceleration limits, overload setting, short-circuit protection and local disconnect location
- Run feedback, fault feedback, permissives, restart behaviour and the mechanical hazards that remain after a stop
For each sensor, switch, valve and actuator, record its tag, location, signal type, normal state, fail-safe state, operating range, calibration interval, cable route and the exact permissive or alarm it supports.
“Motor unavailable” is not enough; HMI diagnostics should distinguish guard open, low level, valve failed to prove, drive fault, overload trip and safety circuit not reset.
| Motor data | Field-device data |
|---|---|
| Tag and duty | Tag and measured condition |
| FLA, protection and starting method | Signal type, range and fail state |
| Feedback and restart rule | Permissive, alarm and safe response |
Use the map to check motor protection separately from short-circuit protection, and confirm the panel SCCR against prospective fault current; UL 508A Supplement SB provides a recognised calculation method. Specify Safe Torque Off where a compatible drive needs torque prevention, but retain a lockable disconnect for isolation and stored-energy control.
Maxwell Tech Solutions Pvt Ltd can use this schedule to expose missing I/O, unsafe restart assumptions and incorrect panel ratings before fabrication.
Frequently asked questions
How does a PLC panel coordinate separate machines?
It reads sensors, checks permissives and interlocks, then sends sequenced commands to motors, valves, conveyors and other actuators.
What should each panel and drive be responsible for?
The PLC handles process decisions and sequencing, while drives control motor speed, acceleration, braking, current limits and drive-specific faults.
How should a safe start, run, trip and restart sequence work?
Confirm utilities, guards, permissives and downstream readiness before starting; stop affected equipment on a trip and require fault clearance and a deliberate restart command.
Which safety functions need more than ordinary PLC logic?
Emergency stop, guard monitoring, safety interlocks and safe torque off require safety-rated devices or safety PLC functions rather than standard control logic alone.